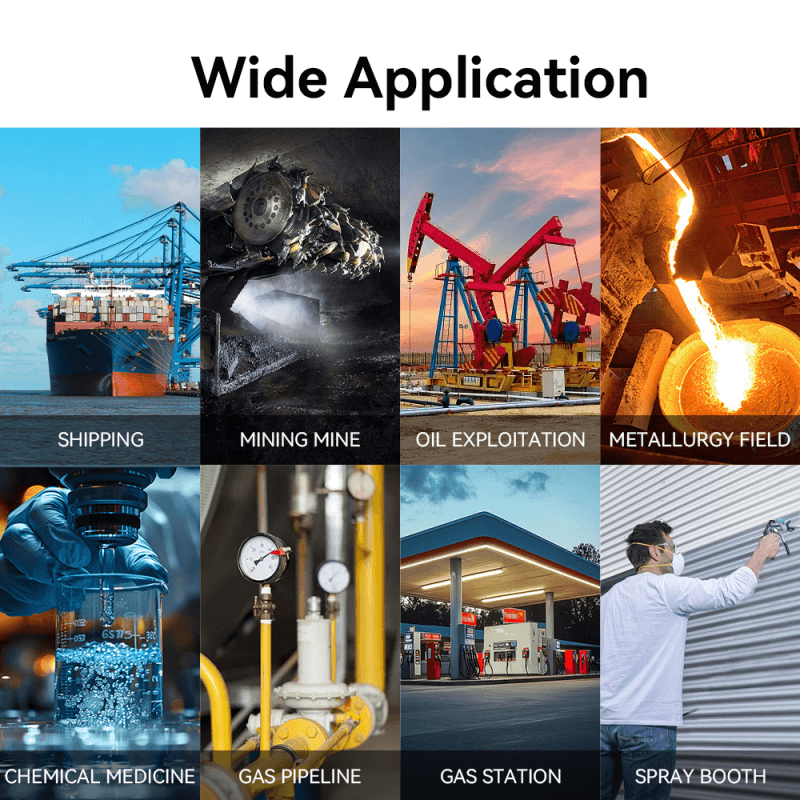
Midway through a furnace shift, an inspection can take a worker away from a monitored workstation and into a space with a different airflow pattern. Gas detection in a steel mill or foundry therefore starts with the gases each operation can release, then separates monitoring at fixed workstations from checks that move with a task.
Production records offer a practical starting point. Furnace operation, a boiler check, and an inspection after maintenance can put people in different places at different times. An industrial gas detector can cover a defined part of that work, provided its sensor, location, and sampling method suit the exposure being evaluated. Shift records preserve that connection when the crew changes.
What the Operation Can Release
Incomplete combustion can produce carbon monoxide in equipment such as smelting furnaces, kilns, and boilers. A furnace operator and a technician checking the combustion equipment may encounter different air conditions even on the same shift. Sulfur dioxide has a different origin in this context. It can be released when sulfur-bearing fuel is burned or during the processing of sulfur-containing minerals.
Knowing the fuel and process gives the site a reason to investigate a particular gas. The detector still needs a channel configured for that gas, with readings expressed in the correct units. An electrochemical carbon monoxide channel, for example, can report carbon monoxide in parts per million. The displayed number belongs to that channel and the air reaching it.
Before approaching a gas detector manufacturer, a plant can describe where each suspected release could occur and which activities bring workers near it. Such a description gives a supplier enough context to discuss sensor options. It also lets the plant review its coverage when a fuel, process, or work route changes, using a concrete record of the original assumptions.
What a Fixed Point Actually Observes
Around a continuously staffed furnace station, a fixed industrial gas detector gives operators a reading from a known point. Where that point is placed matters because furnace openings, local exhaust, and work locations determine which air reaches the sensor. Even two points in the same bay can observe different conditions when ventilation moves air along different paths.
Configured for carbon monoxide or sulfur dioxide, a Bosean BH-60 fixed transmitter offers a standard 4–20 mA output. The installed gas configuration determines what the signal represents. A receiving channel needs the corresponding gas name, units, and range so a reading can be traced back to the right transmitter and interpreted at the control point.
An installation review can use the selected model documentation from the gas detector manufacturer alongside the plant’s equipment register. Matching the transmitter tag and receiving channel to the location gives operators a clear reference when investigating a changing reading. The register is also useful after servicing, when a crew needs to establish which point has returned to operation.
Covering Inspection and Service Routes
Once a technician leaves the station, the fixed reading describes conditions back at its installed point. A portable industrial gas detector can follow the work route so readings can be related to the position of the worker. In diffusion mode, the instrument responds to the surrounding air that reaches its sensor during the task.
Some checks call for collecting air from a point away from the instrument. Natural diffusion and pumped sampling are both available on the Bosean S40, which supports configurations for up to four gases. The pump is rated at 500 mL/min, and the device can indicate a pump fault. That warning is relevant to whether the intended sample reached the instrument.
With pumped sampling, a field record can distinguish the point where air was collected from the place where the person held the instrument. That distinction becomes useful when an inspection changes direction or pauses between two locations. Sampling arrangements serve the planned check, while the site’s work procedures govern how access and any interruption of the task are handled.
Carrying Readings Into the Next Shift
Location and task details make a gas reading useful beyond the moment it was taken. A handover can pair the time and gas channel with the fixed point tag or portable sampling position, then describe what the equipment and ventilation were doing. If two readings differ, those details give the incoming crew a way to investigate the difference.
Where a station uses a Bosean fixed transmitter and the roving team carries a portable unit, the model and channel names help distinguish the two records. A question about the meaning of a device status can then go to the gas detector manufacturer with the instrument configuration and the status as it appeared on the display.
Open items deserve an owner in the handover. A point taken out of service or a sampling check interrupted by a pump warning can be listed with the person following it up. The next operator then knows which readings were available, which checks were interrupted, and what remains to be measured.
Together, these records make the coverage of a shift understandable. Before the next round, the incoming crew can use the open items to identify which planned checks depend on equipment that is still unavailable. The useful handover is one the incoming crew can act on while the circumstances behind each reading are still clear.
SEO Title: Gas Detection in Steel Mills and Foundries
Meta Description: See how steel mills and foundries use fixed monitoring points and portable detectors to cover process areas and record readings across shifts.
